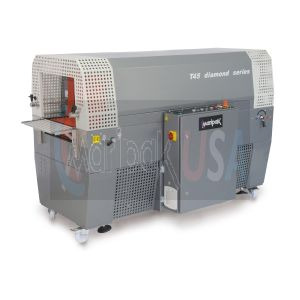
Industrial packaging facilities require robust, high-speed finishing equipment to deliver professional, tamper-evident product seals consistently. Integrating high-performance thermal shrinking technology into existing conveyor lines ensures uniform film contraction across diverse product dimensions. Utilizing engineered heat shrink tunnels provides precise digital temperature control, bottom-embedded heating chambers, and adjustable airflow flaps to prevent film distortion. Heavy-duty double-layered isolation chambers retain internal thermal energy, drastically reducing power consumption while accelerating processing speeds. Upgrading end-of-line packaging infrastructure with automated thermal systems shields products from environmental damage, enhances shelf presentation, and optimizes daily warehouse throughput.
Key Advantages of High-Performance Industrial Shrink Equipment
Investing in commercial thermal packaging systems delivers substantial operational, financial, and mechanical benefits for modern manufacturing operations. Understanding core airflow dynamics helps plant managers select equipment configurations tailored to their specific film materials.
- Precision PID Temperature Control: Maintains accurate internal heat levels to prevent burning or under-shrinking delicate films.
- Double-Layered Thermal Insulation: Minimizes ambient heat loss, protecting surrounding operators while cutting daily energy overhead.
- Variable Conveyor Speed Drive: Synchronizes product flow with upstream sealers to ensure complete, wrinkle-free film contraction.
- Multi-Film Material Compatibility: Adapts instantly between polyolefin (POF) and polyethylene (PE) wrapping films via adjustable systems.
Deploying dependable heat shrink tunnels ensures your fulfillment center operates at peak throughput while maintaining exceptional product finishing standards.
Streamlining Inline Packaging Workflows and Thermal Calibration
Synchronizing Infeed Conveyors with Thermal Chambers
Integrating automated heat tunnels directly alongside l-sealers or side-sealers eliminates manual handling bottlenecks between wrapping stages. Continuous mechanical motion feeds wrapped bundles smoothly into the heated chamber, maintaining uniform spacing for balanced air circulation.
Selecting Premium Industrial Machinery Solutions
Evaluating available automated hardware options requires matching chamber dimensions, belt styles, and wattage capacities to your facility’s volume. Integrating versatile heat shrink tunnels into active packaging operations allows facility operators to scale order fulfillment seamlessly. Advanced touchscreen controls simplify recipe management, permitting fast transitions between varying product sizes.
Safety Protocols and Energy-Saving Engineering
Maintaining safe operational conditions across industrial heat chambers requires automated safety mechanisms that protect equipment and personnel. Built-in automatic cool-down cycles prevent heat damage to internal blower fans and conveyor belts prior to complete system shutdown.
Emergency temperature cut-offs, conveyor jam sensors, and protective safety shields minimize operational hazards during continuous production shifts. Internal airflow adjustments allow operators to direct heat precisely where required, maximizing film contraction efficiency.
Choosing top-tier heat shrink tunnels protects your production floor against unexpected downtime and unsafe thermal exposure. Rugged steel chassis construction ensures stable performance through demanding multi-shift commercial schedules.
Sourcing Commercial Packaging Equipment for Scalable Facilities
Accessing specialized packaging machinery ensures your production facility benefits from certified engineering standards, long-term warranties, and rapid spare parts availability. Connecting with reputable industrial equipment providers links facility managers with innovative heat tunnels, expert technical installation, and ongoing maintenance support.
Upgrading your secondary packaging lineup with industrial-grade equipment ensures consistent package integrity across all distribution channels. Professional guidance assists in selecting the ideal tunnel dimensions and conveyor belt configurations for your application.
Conclusion
Maximizing product protection and packaging presentation requires investing in high-performance thermal shrink technology built for continuous industrial demands. Finding a reliable shrink wrap machine for sale through specialized manufacturing suppliers guarantees access to energy-efficient heat chambers, intuitive digital controls, and dedicated technical support. Upgrading your secondary packaging infrastructure streamlines order processing, lowers labor costs, and elevates your brand’s unboxing experience. Explore advanced thermal packaging solutions today to transform your facility’s operational productivity.
